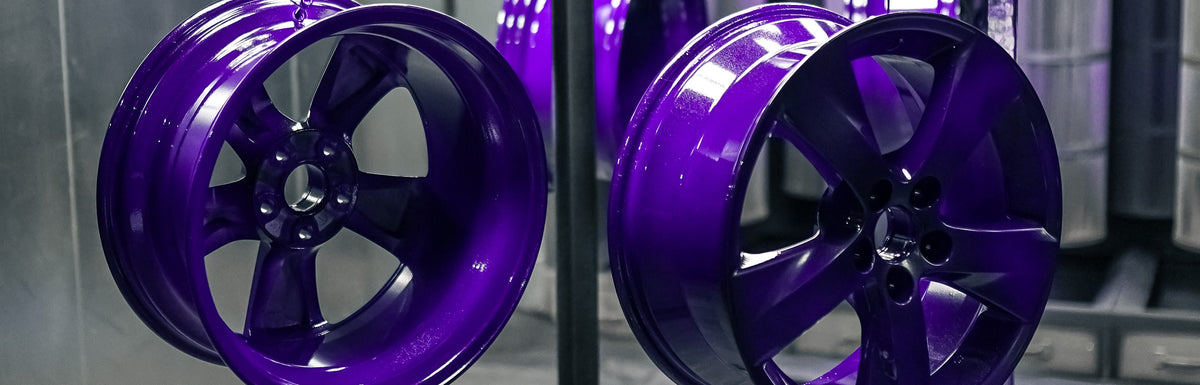
Look inside an enclosure, at the bottom of a U-shaped extrusion or in the hollow between two spokes of a wheel: these are the places where powder has the hardest time settling. The phenomenon has a name, the Faraday cage effect, and it explains a good part of an applicator's know-how.
Where the phenomenon comes from
The gun charges the powder and creates an electric field between its tip and the grounded part. This field concentrates on the edges of a recess, which are closer to the gun: the powder builds up there instead of going in to the bottom, as PCI Magazine explains. The air that carries the powder also works against us: when it is too strong, it blows the powder back out of the recess, notes Products Finishing.

The settings that help
The reflex of turning up the power makes the problem worse. The sources agree on the direction, even if their numbers vary: limit the gun current, reduce the conveying air, choose a flat spray nozzle for narrow passages and keep your distance. Recent guns have modes designed for this. Gema adjusts the current in steps of half a microamp at low settings, and Nordson offers programs for deep cavities. Good grounding is also needed: a doubtful contact amplifies the effect.
Too much powder also hurts
Insisting on a recess has a price. When too much charged powder builds up, it repels the powder that arrives. The Powder Coating Institute puts this threshold at around 4 to 5 mils, or 100 to 125 µm. The defect shows after curing: an orange peel surface. On a second coat, the organization advises reducing the voltage by at least half.
What this changes for your parts
On a complex part, the applicator coats the recesses first, then the easy surfaces. It is a matter of hand and experience. The way the part is hung matters just as much: it determines the angles the gun can reach. If an area absolutely must be covered, or on the contrary must stay bare, say so in your quote request.
In summary
- The electric field concentrates on the edges: powder avoids inside corners.
- The fix is to limit the current and the air, not to turn up the power.
- Too much powder causes repulsion and orange peel.
- How the part is hung and the order of application make the difference.